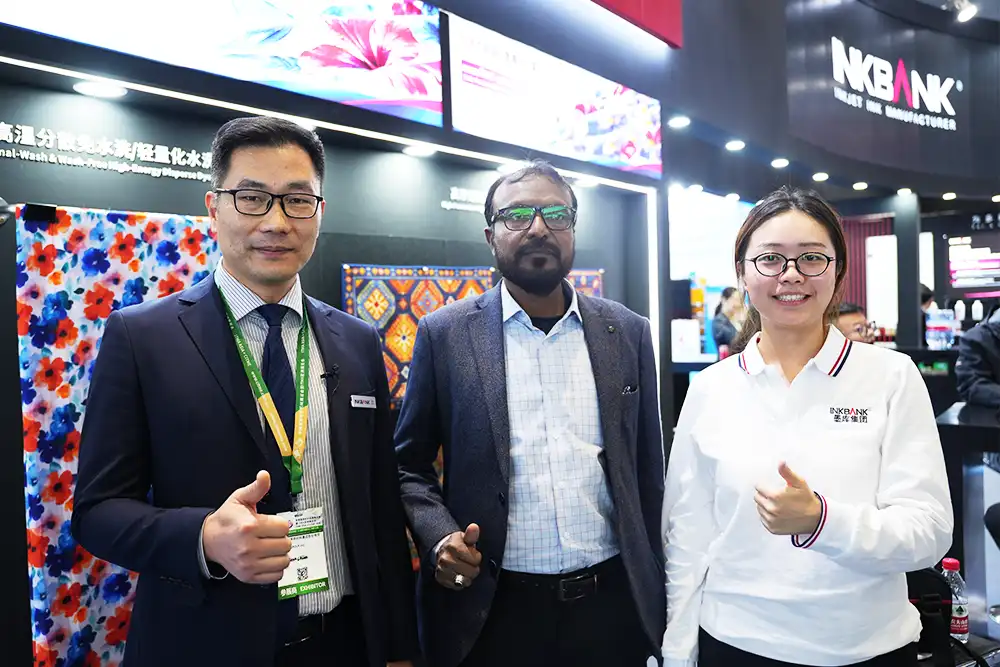
INKBANK Group, a China-based manufacturer of digital inkjet inks and printing solutions, is highlighting its advanced textile printing ink technologies at ITMA ASIA + CITME 2026, taking place from November 20–24 at the National Exhibition and Convention Center (NECC) in Shanghai.
As the exhibition brings together global textile machinery manufacturers and technology providers, INKBANK is drawing attention to an increasingly important aspect of digital textile production: the role of ink in achieving consistent quality, operational reliability and sustainable manufacturing.
Four Ink Technologies for Diverse Textile Applications
INKBANK’s participation centres on four digital textile ink technologies: high-energy disperse inks, roll-to-roll (R2R) pigment inks, reactive dye inks and acid dye inks. Each addresses different textile applications and production requirements, reflecting the industry’s growing demand for reliable, efficient and environmentally responsible printing solutions.
With digital textile printing increasingly moving beyond sampling into full-scale industrial production, INKBANK emphasises that ink performance directly affects shade consistency, printhead stability, colour fastness, fabric hand feel and production downtime.
Moving Beyond Ink Price to Production Efficiency
A central message of INKBANK’s technology approach is that ink should be considered a critical part of the manufacturing system rather than simply a consumable.
The company advocates evaluating the true cost of printing per saleable metre, taking into account ink consumption, cleaning cycles, reworking, fabric waste, machine downtime and delivery reliability.
This approach is particularly relevant for export-oriented textile manufacturers facing tighter delivery schedules, smaller production batches and increasingly demanding international buyer requirements.
Research, Quality and Sustainability
INKBANK supports its product development through 16 R&D laboratories and environmental testing rooms, alongside more than 500 test printing units, enabling formulation development and testing across different fabrics, printing systems and operating conditions.
The company’s reported compliance capabilities include GOTS 7.0, OEKO-TEX ECO PASSPORT and ZDHC MRSL 3.1, demonstrating its focus on meeting international textile supply-chain requirements.
With products supplied to more than 100 countries and regions, INKBANK continues to strengthen its position in the global digital printing industry.
Supporting the Next Generation of Textile Manufacturing
As ITMA ASIA + CITME 2026 continues in Shanghai, INKBANK’s presence highlights the importance of integrating ink chemistry, printing equipment and textile finishing processes to achieve more reliable industrial production.
For textile manufacturers seeking greater productivity, reduced waste and consistent quality, INKBANK’s technology portfolio reinforces an important industry message: the future of digital textile printing depends not only on faster machines, but also on smarter, more reliable ink systems.